Technical article
Endress+Hauser Flow Meter Calibration: Why a Certificate Isn't Verification
by Marcus Feld
A quality manager explains the difference between calibration and verification, using Endress+Hauser flow meters, nuclear level transmitters, and the hidden failure modes that certification doesn't catch.
-
Comparison 1: What a Certificate Actually Covers vs. What It Doesn't
-
Comparison 2: The Cost of Verification vs. the Cost of Finding Out Later
-
Comparison 3: What Each Method Is Good At Catching
-
The Cases That Changed How I Review Instruments
-
What I Use Now: A Short Acceptance Checklist
-
When Can You Skip Verification?
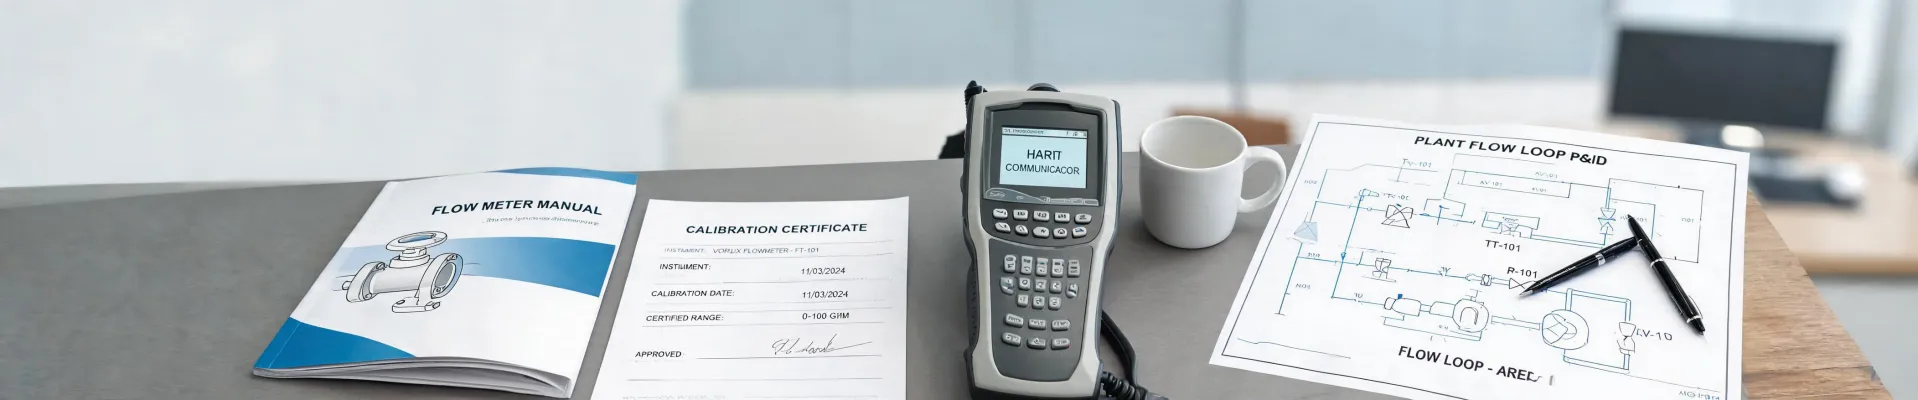
Most people treat a calibration certificate as proof that an instrument works. In my experience, it's proof that an instrument worked—at a specific place, on a specific day, under specific conditions. It is not proof that the exact device sitting on your skid is ready to run today.
I'm a quality manager at a process manufacturing site. I review every instrument that comes through our receiving dock—roughly 400+ unique items a year. In 2024, I rejected around 7% of first deliveries for reasons that had nothing to do with the factory calibration certificate. Tag codes didn't match the order. A HART address was set to the same number as the adjacent transmitter. A configuration file loaded the wrong range. Would those have shown up if we had bolted everything in and trusted the paperwork? Absolutely.
At our site, we specify a lot of Endress+Hauser instruments, so this isn't a knock on their quality. It's a reminder that no brand is immune to transit, storage, and configuration errors.
This article compares two approaches to a new instrument: trusting the certificate, and running a pre-installation acceptance verification. Neither one replaces the other. But once you see the difference, you'll stop treating certificates as a pass to skip the field check.
Comparison 1: What a Certificate Actually Covers vs. What It Doesn't
A calibration certificate, especially one from an ISO/IEC 17025 accredited lab, tells you that the instrument was compared against a reference standard, within tolerance, under controlled conditions. That's valuable. It also tells you almost nothing about this specific unit's journey after it left the calibration bench.
The certificate is a memory. Verification is a current event.
An acceptance verification asks a different question: Does this instrument, as configured and connected, read correctly right now? That's the question the commissioning engineer actually cares about.
Here's the thing people get wrong: calibrated does not mean ready. A brand-new instrument can carry a perfect certificate and still have an incorrect firmware revision, a loose sensor connection, or a configuration that was overwritten during testing.
Comparison 2: The Cost of Verification vs. the Cost of Finding Out Later
Verification has a real cost. You need a technician, a reference device, and time. For a pressure transmitter, maybe 20 minutes. For a flow meter, a full wet calibration can take half a day. On a project with 50 instruments, that's not free.
But compare that with the cost of discovering the problem after installation. The instrument is braced, wired, labeled, and insulated. The line is filled. The skid is certified. Then the reading doesn't match the independent level indication. Now you're cutting insulation, breaking joints, bringing in a crane, and re-certifying the loop.
That exact scenario cost us a $22,000 redo and delayed our launch by three weeks. The lesson stuck with me more than the invoice: prevention is cheaper than correction. Five minutes of verification beats five days of rework.
Comparison 3: What Each Method Is Good At Catching
A factory calibration catches sensor-level problems: a bad linearity curve, an out-of-spec reference element, an electronic board failure. Those are real and important.
What it routinely misses are the handoff problems:
- Wrong tag or range code in the transmitter
- Firmware revision that doesn't match the expected output
- HART address conflicts on a multi-drop loop
- Transit damage that shifts a sensor zero point
- Configuration memory that doesn't match the approved datasheet
- Engineering units set to something the DCS card wasn't expecting
An acceptance verification catches those because it tests the whole chain, not just the sensor.
For example, Endress+Hauser flow meter calibration is not a single activity. A Coriolis meter needs a zero-point check; an electromagnetic meter needs a loop test or wet calibration; an ultrasonic clamp-on meter needs pipe wall thickness and sound speed verification. Each one catches a different type of error.
The Cases That Changed How I Review Instruments
I only believed in pre-installation verification after skipping it once. Several years ago, we received eight flowmeters with valid calibration certificates. We installed them, filled the line, and started the hydrotest. Three of the eight were configured with the wrong velocity range. The certificates were perfect. The instruments were not.
That experience changed how I look at every instrument family:
Nuclear level transmitters. For applications that need a nuclear level transmitter, Endress+Hauser's Gammapilot series is dependable. But radiometric measurement adds a variable that even experienced engineers forget: source decay correction. A certificate might verify the detector, but it won't verify that the decay constant in the configuration matches the actual source age. If that's wrong, you can have a certified instrument giving you a confidently wrong level reading.
Flow meters. For any Endress+Hauser flow meter calibration, I always include a zero-point check. On a Coriolis meter, an unstable zero is one of the fastest ways to spot mounting stress or transit damage. If the zero is stable and the span reads correctly, you can trust the installation.
The same logic follows outside the process line. A centrifuge 5804 in the lab can spin and still be out of calibration. Rotor speed drifts, and a 50 RPM error can change separation results. An optical tachometer check is cheap.
An insulation tester is another classic. It can display a reassuring 500 MΩ while the internal test voltage drops under load. That reading is fiction. Verify it against a known resistor before you use it on a live cable.
And if you're integrating a weighing system, you'll eventually ask: What is Rice Lake weighing systems programming language? The short answer is iRite, the C-like scripting environment used in Rice Lake's 920i and 1280 indicators. Why does that matter here? Because a scale can pass a deadweight test while the batching logic has an error that only appears when two inputs change at once. A good acceptance test exercises the software, not just the load cells.
What I Use Now: A Short Acceptance Checklist
Now every contract I review includes a verification step before installation. The checklist doesn't need to be long:
- Compare the nameplate and HART tag to the approved datasheet.
- Check firmware version and hardware revision.
- Record as-found zero and status bits before touching any configuration.
- Simulate a 4–20 mA signal and confirm the DCS reads it in both directions.
- For flow meters: perform a zero check and, where practical, a wet calibration or loop check.
- For radiometric level instruments: verify the source decay correction and run an empty-vessel simulation.
- For scales: run a deadweight test and then execute the program logic with simulated inputs.
- Save a signed acceptance report with photos of the nameplate and test setup.
- Confirm 24 V loop power at the terminal, not just at the power supply.
- Don't calibrate away a problem. If a new instrument needs more than a trivial trim to read correctly, stop and investigate.
That list has saved us an estimated $8,000 in potential rework since I created it. It's the cheapest insurance I know.
When Can You Skip Verification?
Honestly, only when the consequence of a wrong reading is zero. For a display-only temperature indicator on a buffer tank, maybe. For a custody transfer flow meter, a safety-related level switch, or a recipe ingredient weight, never.
Verify if:
- The instrument was shipped a long distance.
- It sat in storage for more than a few months.
- It's part of a safety or quality-critical loop.
- More than one person touched the configuration.
- The certificate is a printout without a unique serial number or signature.
Trust the certificate alone if:
- It's a direct spare going into an identical existing slot.
- Storage and handling conditions were controlled.
- The risk of a wrong reading is low, and the verification cost is higher than the risk.
I'm not suggesting you stop using accredited calibration labs. I'm saying the certificate is the beginning of confidence, not the end of it. Install the instrument, verify the whole loop, and keep the paperwork in a place you can find when an auditor asks.
Because the most expensive instrument I've ever seen wasn't the one with the highest purchase price. It was the one that worked on paper and failed in service.
Marcus Feld
Marcus Feld is an electrical test and measurement analyst specializing in multimeters, oscilloscopes, clamp meters, insulation testers, spectrum analyzers, and data loggers. He applies IEC 61010-2-030 and IEC 61010-031 concepts while examining measurement category, bandwidth, true-RMS response, input loading, and stated uncertainty. His work helps maintenance engineers and test teams choose safe instruments with performance suited to the signals and environments they actually measure.