Technical article
Endress+Hauser Flow Meter FAQ: Clamp-On Ultrasonic, Electromagnetic, Calipers, and Thermal Cameras
by Marcus Feld
A practical FAQ from a quality reviewer about Endress+Hauser electromagnetic and clamp-on ultrasonic flow meters, dial caliper parts, encoder wheels, and Fluke vs FLIR thermal cameras.
-
How does an Endress+Hauser electromagnetic flow meter work?
-
When should I choose an Endress+Hauser clamp-on ultrasonic flow meter instead?
-
Is an Endress+Hauser clamp-on ultrasonic flow meter accurate enough for flow verification?
-
Why do I need a dial caliper parts diagram? Is an encoder wheel part of a caliper?
-
Fluke vs FLIR thermal cameras: which should an instrument team choose?
-
Does Endress+Hauser support small plants and small orders?
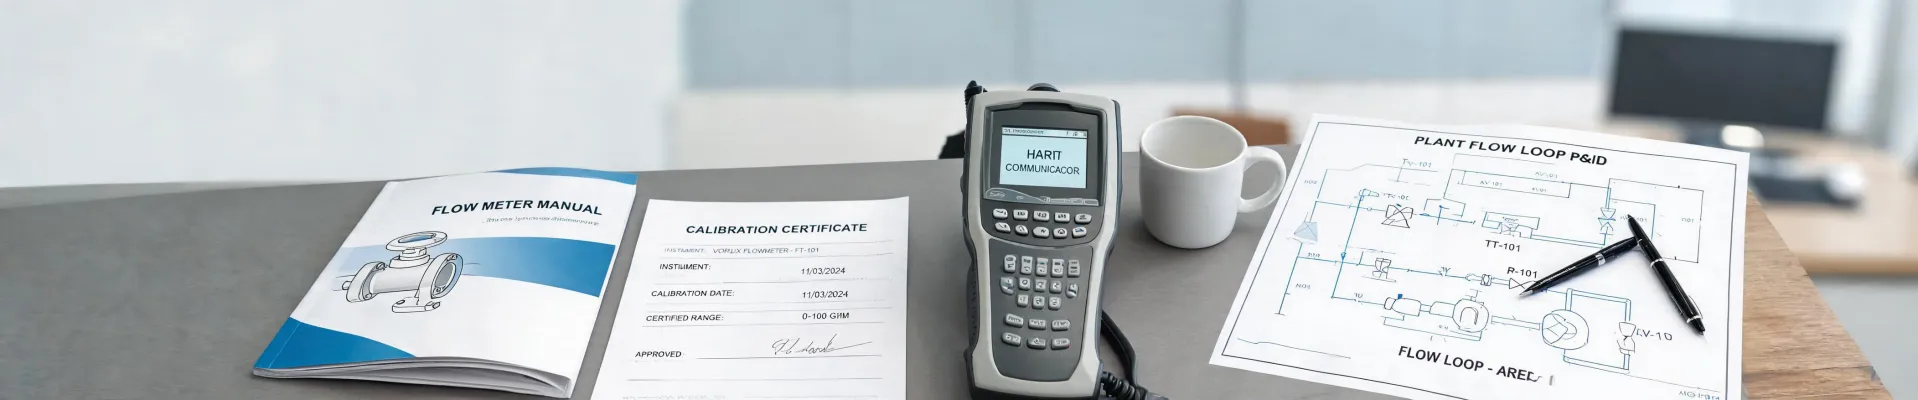
I work on the quality side of process-instrumentation projects. In a normal year I review around 200 calibration certificates, inspection reports, and commissioning records before they go to plant owners. Maybe 180—I would have to check the database. In 2024, through Q3, I rejected roughly 9% of first submittals, usually for unglamorous reasons: a missing grounding strap, a straight-pipe violation, or a thermal photo taken with the wrong emissivity. Here are the flow meter and inspection-tool questions that show up most often in that review process.
How does an Endress+Hauser electromagnetic flow meter work?
Endress+Hauser electromagnetic flow meters—the Proline Promag family in many plants—use Faraday’s law. Coils above and below the flow tube create a magnetic field. When a conductive liquid moves through the field, a small voltage is induced in the measuring electrodes. The transmitter converts that voltage into an average fluid velocity and multiplies it by the pipe cross-sectional area to show volumetric flow.
Because there is no turbine or gear in the bore, a magnetic flow meter has no moving parts and little obstruction. That makes it a reasonable fit for process water, wastewater, acids, and other liquids that should not meet moving hardware.
The condition is that the liquid has to be conductive, and the tube has to stay full. If the meter is installed with the wrong liner, if the line can partially drain, or if the electrode circuit loses its reference, the output can drift. I once found a zero-drift problem caused by missing grounding rings on a PFA-lined meter. The transmitter was fine; the installation was not. Grounding is not optional on an electromagnetic flow meter—it is part of the measurement circuit.
When should I choose an Endress+Hauser clamp-on ultrasonic flow meter instead?
An Endress+Hauser clamp-on ultrasonic flow meter has a different job from an inline meter. The ultrasonic sensors clamp onto the outside of an existing pipe. The meter sends ultrasonic pulses through the pipe wall and liquid, then uses the transit-time difference to estimate flow velocity. It does not require cutting into the line, so the process can continue running during the measurement.
I use that capability for temporary water-balance work, verifying another meter, or checking whether a pump really is delivering the design flow. It is also useful on lines that cannot be taken out of service.
The trade-off is that clamp-on accuracy depends on pipe information and field conditions. Actual outside diameter, wall thickness, lining, liquid type, and temperature all affect the calculation. If someone guesses the pipe schedule, the display can be smooth and confidently wrong.
Is an Endress+Hauser clamp-on ultrasonic flow meter accurate enough for flow verification?
It is accurate enough to find a problem, but I do not treat it as a flow laboratory standard. In my experience, a clamp-on Endress+Hauser flow meter can catch gross errors: a bad sensor on an inline magmeter, a bypass that someone left open, an undersized pump, or a control valve causing an unstable reading.
It can also give a useful comparison when the permanent meter is reading far off. If the inline meter spec says ±0.3% of reading, a clamp-on meter with a larger uncertainty cannot prove that specification by itself. It can show whether the shift is reasonable or whether something needs to be opened and checked.
What I insist on before using the reading as evidence is straight pipe, clean pipe surface, ultrasonic coupling gel, and a verified pipe wall thickness. If the surface is heavily corroded or the pipe has loose lining, I treat the clamp-on values as directional, not conclusive.
Why do I need a dial caliper parts diagram? Is an encoder wheel part of a caliper?
A dial caliper will not calibrate a flow meter, but it belongs in the same quality kit. I use one to check the dimensions of replacement gaskets, sensor mounting brackets, flanges, and clamp hardware before the meter goes into the line. A small fit error on a spacer or bracket can make an expensive sensor unusable.
When you open a dial caliper parts diagram, you normally see the beam, outside jaws, inside jaws, depth rod, dial face, bezel lock, thumb roll, and the rack-and-pinion mechanism that turns the needle. That diagram helps explain why a caliper may read poorly: a dirty rack, bent jaw, or a bezel that has slipped.
If you searched for “encoder wheel” because your caliper is digital, look more carefully. A traditional dial caliper does not have an encoder wheel. Digital calipers usually use capacitive or magnetic linear scales. Rotary encoder wheels are separate components found in motors, positioners, and measuring wheels. The shared point is that both systems convert motion into numbers, and both need the mechanical-to-electrical conversion to be clean.
Fluke vs FLIR thermal cameras: which should an instrument team choose?
I have used both Fluke and FLIR imagers in plants. There is no single “better” brand for every team. Fluke makes sense for a crew already using Fluke electrical testers and software. FLIR has a wide product lineup and mobile software that many new techs find easy to adopt. Both can produce good thermal data if the user understands the tool.
More important than the label is resolution and emissivity. A 160×120 detector can locate missing insulation and a hot breaker. If the team plans to inspect small electronics or small mechanical parts, 320×240 or higher is worth the extra cost.
In a quality audit, images get rejected when emissivity is set to 0.95 on bare copper or aluminum. That is not a Fluke or FLIR failure; it is a training failure. Match the emissivity setting to the surface, and document the reflected temperature when the target is shiny.
Does Endress+Hauser support small plants and small orders?
I won’t promise every distributor responds the same way, and I am not going to claim small orders get factory-direct priority. What I can tell you is that small is not a quality problem. The Endress+Hauser distribution channel is built around real specifications, and the clearer you are, the better the response.
When I first started in this role, I assumed a two-person contractor with a single flow meter request would not get much engineering attention. After several years, I have changed that assumption. The support we see depends on the completeness of the request, not the size of the PO.
A small plant can get the same technical detail as a large plant when it sends line size, pipe material, fluid conductivity, pressure, and signal output requirements. That is also true for replacement parts or a clamp-on flow meter rental. Get the pipe schedule and process conditions into the first message, and ask for the same evidence you would require from any supplier: description of scope, accuracy statement, lead time, and spare parts availability.
Marcus Feld
Marcus Feld is an electrical test and measurement analyst specializing in multimeters, oscilloscopes, clamp meters, insulation testers, spectrum analyzers, and data loggers. He applies IEC 61010-2-030 and IEC 61010-031 concepts while examining measurement category, bandwidth, true-RMS response, input loading, and stated uncertainty. His work helps maintenance engineers and test teams choose safe instruments with performance suited to the signals and environments they actually measure.